The value of a mixing tank is not the volume it holds but the steadiness it delivers downstream. One recipe at one bulk density lets the feeder hold a single setting, and that decision reaches all the way to the accuracy of the finished batch.
Follow the chain backwards from the pellet and the reason for the tank becomes clear. Film flake and rigid flake differ several times over in bulk density and moisture; blend them or the feeder spends the shift correcting for layers that should never have reached it.
Why feed uniformity comes first
- The tank sits downstream of the dryer and upstream of the force feeder, never ahead of the dryer.
- Washed film is 30-80 kg/m³ against 250-400 kg/m³ for rigid flake, so unmixed feed starves the screw.
- A gravimetric feeder holds 0.25 to 0.5% but still needs a blend that arrives mixed rather than in layers.
- Sample the discharge across a whole batch by weight; the average alone hides a layering failure.
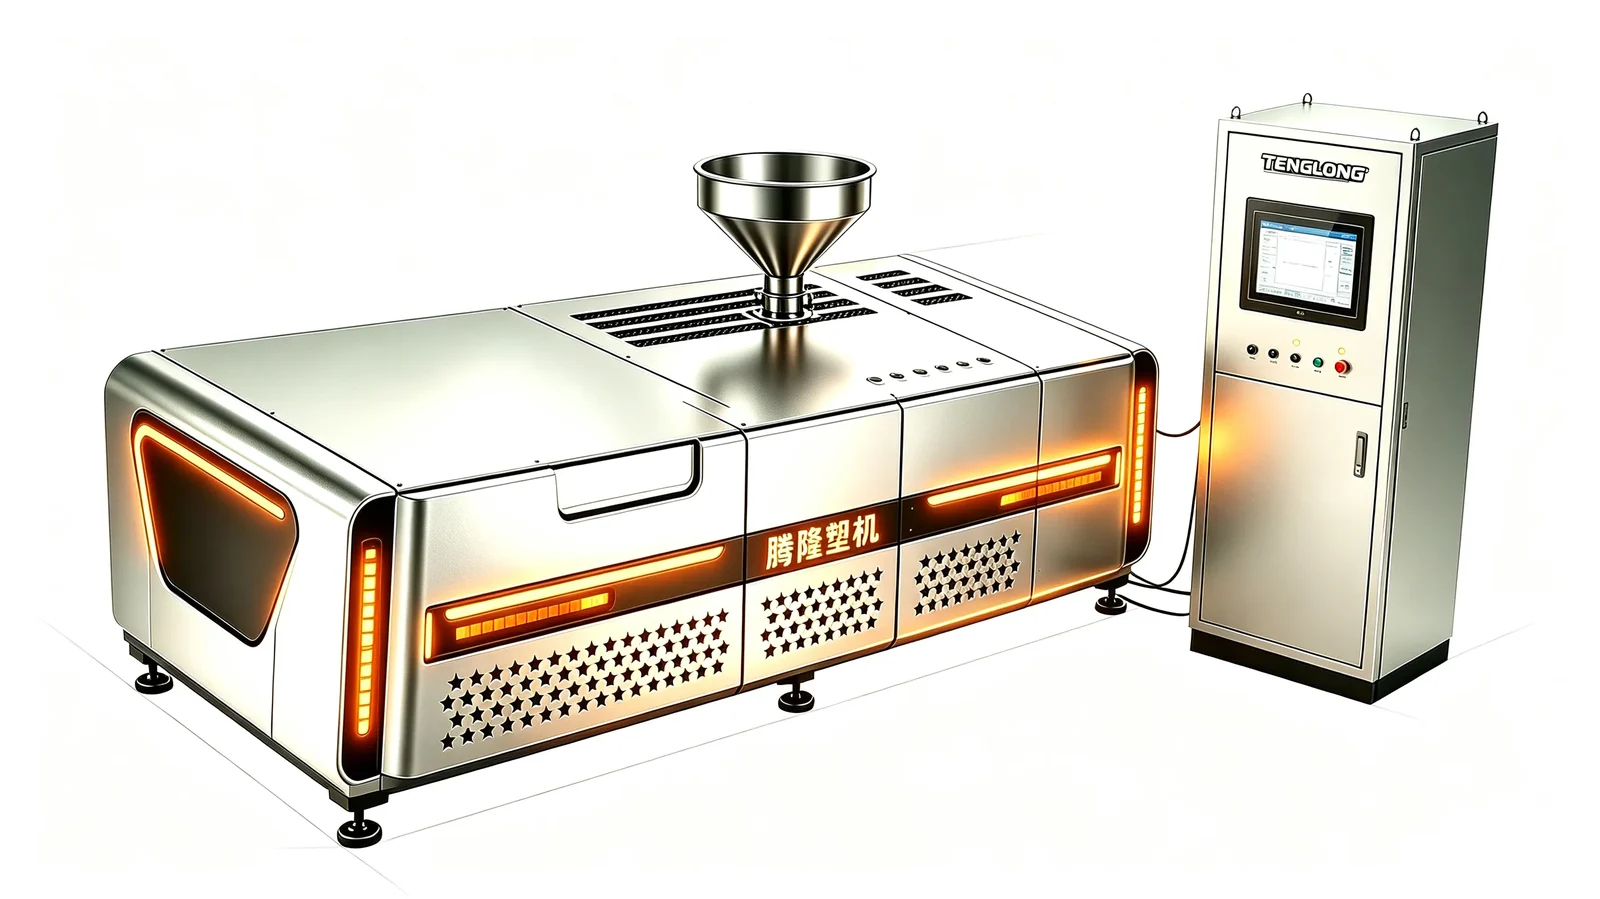
One decision, followed all the way to the pellet
A mixing tank blends flake, powder and colour so the extruder sees a consistent bulk density and a consistent recipe, and it removes the need to blend by hand at the hopper. That single purpose reaches further down the line than the vessel itself, because every feeding device after it is calibrated against what it receives.
The tank sits between the drying stage and the force feeder, so the extruder receives one recipe at one bulk density. Move it ahead of the dryer and it mixes wet material, which then dries unevenly; move it too far from the feeder and the blend can separate again in the intervening pipework.
This is why the vessel should be judged by what it delivers rather than by its volume. A high speed mixer is available from 5 litres to 2,000 litres including hot and cold two stage designs, but a tank that holds the right number of litres and delivers layers instead of a blend has failed its only real test.
Bulk density is the hidden variable in the recipe
The two common feedstocks differ sharply: light washed film sits in a low density band and arrives far wetter, while rigid flake is several times denser and much drier. Feed the extruder a recipe whose proportions swing by that much and no feeder setting can hold the recipe steady.
Compare the two feeder classes on accuracy and price. A volumetric unit costs US$2,000-8,000 at plus or minus 1 to 2%, while a gravimetric unit costs US$8,000-25,000 at plus or minus 0.25 to 0.5% and corrects for density on its own. Either way the blend still has to arrive mixed rather than in layers.
The point is that a feeder measures what is in front of it. If the tank has delivered a layer of light film followed by a layer of heavy flake, the feeder is reading a moving target and correcting for a change that should never have reached it. Uniformity upstream is cheaper than accuracy bought downstream.
Where in the line the tank belongs
The tank has to be downstream of the dryer and upstream of the force feeder, and a tank placed before the dryer mixes wet material and dries it unevenly. Sequence is not a matter of layout convenience here; it is the difference between a recipe that holds and a batch that drifts.
Humidity and residual water change the mass in a volumetric cup without changing its volume, so a tank that blends before drying hands the feeder a material whose apparent weight keeps changing. Dry first, then blend, is the order that keeps both the recipe and the moisture figure stable.
The same logic reaches the screw. Low-density film flake starves a screw that has been set for rigid flake, and the force feeder is there to push it in. A blend that holds its bulk density lets the feeder work at one setting instead of chasing the difference between film and flake every few minutes.
How to prove the blend is actually uniform
Pull a handful from the discharge at short intervals through a full batch and compare colour, texture and mass. Put each sample on a scale instead of trusting your eyes: a tank that delivers layers has failed even when the batch average looks right on paper.
A gravimetric batch blender runs from 260 kg/h maximum throughput with a 3 kg batch and a 0.15 kW stirring motor up to 4,850 kg/h with a 90 kg batch and a 2.2 kW motor, on 4-6 bar compressed air with four hoppers and one screw rod per hopper. Whatever the scale, the proof is the same: sample across the batch, not at the start of it.
A free test on 10-20 kg of the buyer’s own material, with video, measured output, specific energy and pellet photos sent before the balance is paid, is the point at which this should be settled. A refundable deposit if the agreed output is missed by more than 5% puts a number on a claim that would otherwise be a brochure sentence.
What it costs when the feed is not uniform
The first cost is the feeder. A plant that cannot hold a recipe often buys a gravimetric feeder at US$8,000-25,000 to fix what a correctly placed mixing tank should have handled, and the feeder then compensates for a problem that is still arriving in layers.
The second cost is the off-spec batch. One ingredient dropping out of the recipe changes the colour or the additive level in every pellet made until somebody notices, and the material already produced cannot be corrected by adjusting the tank afterwards.
The third cost is the operator. Manual blending at the hopper ties a person to the line and reintroduces the variation the tank was bought to remove. The tank pays for itself by removing that person from the loop and by letting the feeder read a steady bulk density all shift.
What changes when the feed is uniform
The table sets out what changes when the feed is uniform. Follow it from the hopper to the batch average the customer receives.
| Feed condition | What the feeder sees | Consequence for the batch |
|---|---|---|
| Washed PE film, 30-80 kg/m³ | Light, variable bulk density at 50-70% moisture | Volumetric dosing drifts as the layer changes |
| Rigid flake, 250-400 kg/m³ | Dense, steadier feed at 30-40% moisture | One feeder setting holds through the batch |
| Volumetric feeder | Plus or minus 1 to 2% stated accuracy | Cheaper, but follows density changes |
| Gravimetric feeder | Plus or minus 0.25 to 0.5%, compensates for density | Costs more, corrects after the fact |
| Tank downstream of dryer | One recipe at one bulk density | No layering, no manual blending at the hopper |
What buyers ask us before they order
Q1: Where should a mixing tank sit in the line?
Downstream of the dryer and upstream of the force feeder. A tank placed ahead of the dryer blends wet material that then dries unevenly, and the feeder inherits a bulk density that keeps changing. Dry first, then blend.
Q2: Does a gravimetric feeder remove the need for mixing?
No. It compensates for density changes after they arrive, at plus or minus 0.25 to 0.5% accuracy, but it cannot turn a separated layer into a recipe. A uniform blend upstream is cheaper than buying accuracy downstream to chase the variation.
Q3: Why do film and rigid flake not mix by density?
Washed PE film sits at 30-80 kg/m³ while rigid flake sits at 250-400 kg/m³, and they enter the line at 50-70% and 30-40% moisture. Without a tank the screw sees layers rather than one recipe, and the output follows those layers.
Q4: How do I prove the blend is uniform?
Sample the discharge at short intervals across a full batch, weighing each handful for colour, texture and mass. Judge the batch by those samples, not by the average, because a tank that delivers layers fails even when the average looks right.
Also worth reading: washing line, glossary, film granulating line and quality control.
Three more notes from the same test floor: Mixing Tank: What It Contains and Why Feed Must Be Uniform, Bulk Density: The Specification That Decides the Blend, Sizing a Mixing Tank and What It Costs and Mixing Tank Acceptance, Commissioning and First-Week Faults.
About the author
Zhou Gong (周工) works on the screw and barrel line at TENGLONG Plastic Machinery, which began in 2016 as a workshop serving recycling plants around Linyi and now ships 820-plus lines to 46 export markets. I take a handful from the discharge at the start, the middle and the end of a trial, because a blend that only looks right at the beginning is the one that costs a customer a batch. Nothing in this article is rounded up from a brochure: every figure was read off a machine or carries the date on which it was published.
Describe the material, the contamination and the output you need, and our engineering team will answer with a model and a price range inside one working day. The trial on 10-20 kg of your own material is free, and a measured output more than 5% under the agreed figure leaves the deposit refundable.