A cubic pellet feeds better than a round one because its flat faces slide over each other in a hopper instead of locking into an arch. A strand pelletizing line makes that cube by cooling strands in a water bath and cutting them with a twelve-blade rotor, holding 2 to 4 mm to plus or minus 0.2 mm.
The shape is not the only reason. The melt path on a strand line is visible, so an operator sees a bubble or a dark speck before it becomes a whole batch of rejects. The price is floor length: 8.5 to 12.5 m from die face to bagging station, against a much shorter die-face line.
What the cube actually buys you
- Flat faces slide in a conical hopper and resist bridging, especially at small sizes.
- A defined pellet volume makes dosing by count or weight repeatable batch to batch.
- The visible melt path lets an operator divert contaminated material before cutting.
- The trade-off is 8.5 to 12.5 m of floor length and more operator attention.
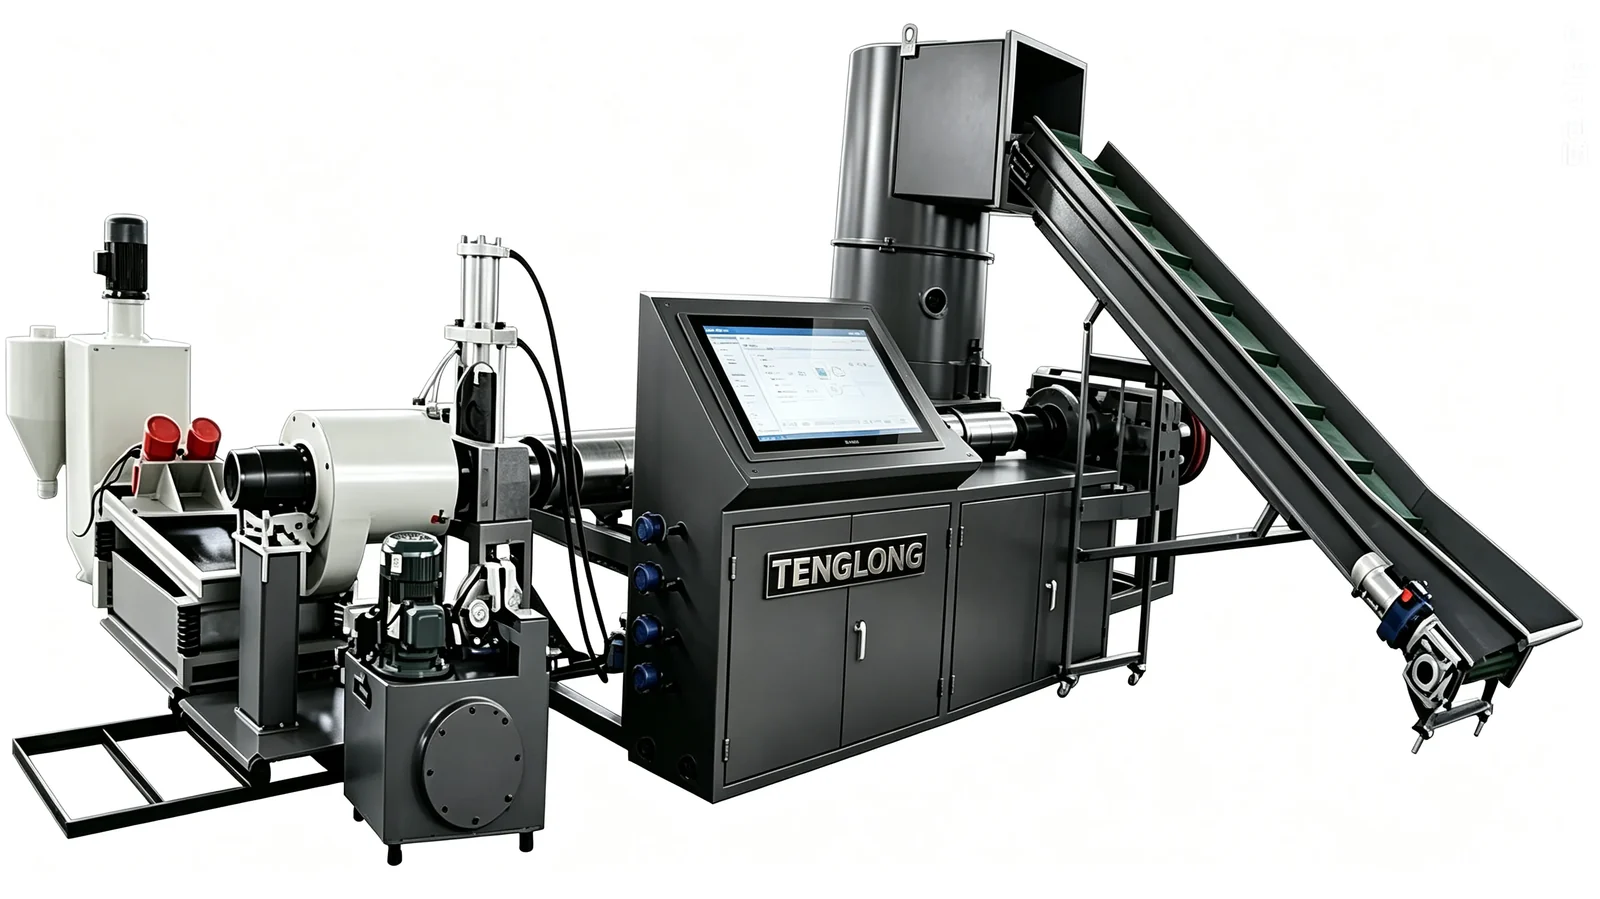
The shape a hopper can actually feed
Ask an injection moulder what shape they want and the answer is usually a cube. That preference is not habit. A cubic pellet made on a strand pelletizing line has flat faces and sharp edges, so it slides over itself in a conical hopper instead of locking into an arch. Round pellets can bridge, especially at 2 mm and below, and a bridged hopper is a press that runs empty while the operator watches.
The second reason is predictability. A cube has a defined volume and a defined length, so the number of pellets per gram is repeatable batch to batch. When a moulder sets a let-down ratio by count rather than by weight, that repeatability removes one variable from the process. Round pellets vary more in their packing fraction, and the variation shows up in dosing.
None of this makes round pellets wrong. It explains why the reference line for injection-grade regrind is still a strand cutter with a water bath, an air knife and a rotating blade. We build that line as the TL-ST platform at 150 to 800 kg/h, and the specification includes 2 to 4 mm cubic pellets held to plus or minus 0.2 mm. That tolerance is what makes the shape useful rather than merely traditional.
What happens between the die and the bag

Melt is pushed through a multi-hole die with eight to twenty-four holes, and the strands fall into a water bath at a shallow angle. The bath is long enough to freeze the core, which takes eight to fifteen seconds at 20 to 35 degrees C. A short bath leaves a soft centre and the cutter smears instead of cutting, so the pellets come out with tails rather than clean faces.
An air knife strips the surface water before the strands reach the feed rolls. That step matters more than it looks: water carried into the cutter makes pellets clump in the bag, and clumped pellets are exactly what a hopper cannot feed. The feed rolls then pull the strands into a twelve-blade rotor running at 200 to 600 rpm, and the cutter produces the cube.
A pneumatic strand-break detector watches the strands and stops the feed within half a second if one breaks. Without it, a broken strand lets melt pour into the bath, and cleaning a flooded bath costs far more than the detector does. The visible melt path is the real advantage of this method: an operator sees a bubble or a contamination speck before it reaches the cutter.
Where a cube beats a round pellet
Injection and extrusion feeding is the first case. The cube releases from a hopper at a consistent rate, and the flat faces give the screw a uniform feed cross-section. For a shop running the same grade eight hours a day, that consistency is worth more than a slightly lower capital cost.
Visual quality control is the second case. On a strand line the melt is visible before it is cut. A dark speck, a bubble or a change in strand diameter is obvious at the bath, and the operator can divert the material. On a die-face system the same fault is only visible in the finished pellet, by which time a whole batch is affected.
Masterbatch with many colours and low output is the third case. Changeover on a strand line is quick to verify because the strand itself shows when the purge is clean. That is why the TL-MB masterbatch granulator uses strand cutting as standard, with underwater cutting offered only for 1.5 mm micro-pellets or pigment systems that smear in a strand bath.
The price of the shape
The trade-off is floor length. A strand line needs eight to twelve metres from the die face to the bagging station, and that is before the extruder itself. The TL-ST-200 occupies 8.5 by 1.2 m, the TL-ST-400 10.5 by 1.4 m, and the TL-ST-800 12.5 by 1.6 m. A water ring line doing the same output fits in roughly half that space.
The second cost is operator attention. Strands can break, the bath needs temperature control, and the air knife needs checking. A line designed for 24/7 duty still has a blade check every eight hours. For a plant with limited floor staff, a die-face cutter removes a set of tasks rather than just a set of components.
Fines are the third consideration. Strand cutting produces the most dust of the three common methods: 0.5% fines is normal and 2% is a maintenance signal. If the customer is a film extruder who cannot tolerate dust in the hopper, that number matters more than the shape advantage.
How to specify the cube
Start with the receiving process, not the cutter. If the pellets go into an injection press, 3 mm is the default size in our published range. Film and cable customers often ask for 2.5 mm, and large mouldings can take 4 mm. The TL-ST cutter reaches all three from the same twelve-blade rotor because pellet length is set by the feed-roll speed ratio, not by blade geometry.
Then fix the tolerance. Plus or minus 0.2 mm is the published figure for strand cutting, and it is tight enough for dosing work. Below 2 mm the cutter output drops and fines rise, so a sub-2 mm requirement should be treated as a special case with a sample run first.
Finally, state the shape in the contract as a measured property: pellet length, diameter, tolerance and maximum fines. A buyer who writes only ‘3 mm pellets’ leaves the definition to the supplier, and two suppliers will not mean the same thing by it. Our own comparison of twelve platforms and our granulator types page both set the shape question out in more detail.
Cube versus round pellet in feeding
Pellet shape is a feeding decision before it is a cutting decision. The table starts from the receiving process and works back to the cutter.
| Property | Strand cube | Die-face round |
|---|---|---|
| Hopper release | Flat faces slide, low bridging | Can arch at 2 mm and below |
| Volume per pellet | Repeatable batch to batch | Packing fraction varies more |
| Size tolerance | +/- 0.2 mm published | About +/- 0.15 mm underwater |
| Fines | 0.5% normal, 2% signals wear | Lower |
| Floor length | 8.5 to 12.5 m | Shorter, no bath |
Frequently asked questions
Q1: Why do injection moulders prefer cubic pellets?
Cubes have flat faces and slide over one another in a conical hopper. Round pellets can lock into an arch, especially at small sizes. A cube also has a repeatable volume, so dosing by count or weight stays consistent from one batch to the next.
Q2: What pellet size should I order for a strand line?
Three millimetres is the default for injection and blow moulding. Film and cable customers often specify 2.5 mm, while large mouldings can use 4 mm. The same cutter reaches all three sizes by changing the feed-roll to cutter speed ratio.
Q3: Does strand cutting make more dust than underwater cutting?
Yes. About 0.5% fines is normal on a strand line and 2% is a maintenance signal. Underwater cutting produces less dust because the pellet is cut submerged. If dust in the hopper is a rejected quality, a die-face system is worth considering.
Q4: How long does a strand line take to install?
A TL-ST line has a published lead time of 20 to 25 days. The line itself occupies 8.5 to 12.5 m depending on output, measured from the die face to the bagging station. Allow another metre at the end for bag access.
Related pages on this site: the twelve-platform comparison.
If you are working through the same machine family, these are the other Strand Bath Length and Water Temperature Explained, Strand Breaking at the Die: From Symptom to Cause, Strand Cutter Maintenance: Knife Clearance and Blades and Strand Pelletizing Line: How Much Floor Space to Plan.
About the author
Zhou Gong (周工) is a recycling machinery engineer at TENGLONG Plastic Machinery in Linyi, Shandong, where 30-plus staff work across 18,000 m² and 12 machine platforms covering 100 to 3,000 kg/h. On every strand line I commission, I watch a sample pour from a bag into a funnel. If it stalls, no downstream machine will fix the shape. Every figure used here has been measured on a machine or taken from a dated published source, not from a brochure.
Send the material form, the contamination level and your target output to our engineering team and you get a model and a price range within one working day. A test run on 10–20 kg of your own material is free, and if the measured output misses the agreed figure by more than 5%, the deposit is refundable.