Bath length on a strand line is set by output, not by available floor space. A 4 m bath suits 150 to 250 kg/h, 5 m suits 350 to 500 kg/h and 800 kg/h needs 6 m, because the core of the strand has to freeze in eight to fifteen seconds before the cutter arrives.
Water temperature is a window from 20 to 35 degrees C. Below 18 the strands turn brittle and snap at the first guide roll; above roughly 40 the core stays soft and the cutter smears. A chiller is offered to hold the window to plus or minus 1 degree through seasonal changes.
The two numbers that set pellet quality
- Bath length follows output: 4, 5 and 6 m for the three TL-ST models.
- The core freezes in eight to fifteen seconds at 20 to 35 degrees C.
- Cold water below 18 degrees makes strands brittle at the first guide roll.
- An air knife strips surface water so pellets do not clump in the bag.
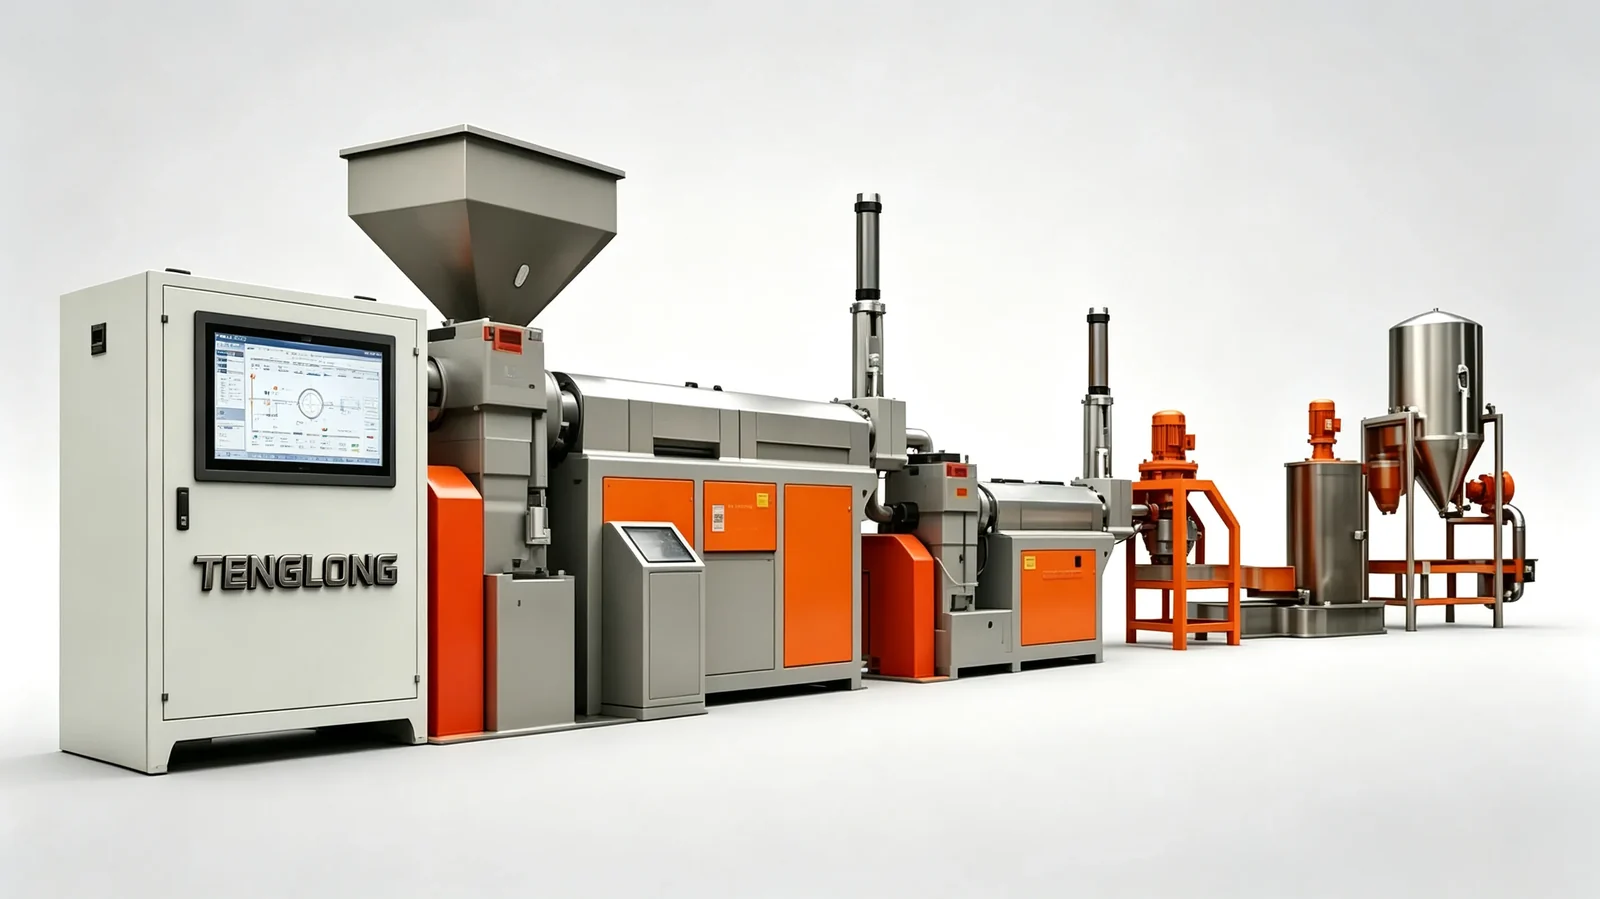
The bath is a heat exchanger, not a trough
The water bath on a strand pelletizing line has one job: freeze the core of the strand before the cutter reaches it. Surface cooling happens in seconds, but the centre of a 3 mm strand holds heat much longer. If the core is still soft when the blades arrive, the cutter does not cut. It presses a soft cylinder flat and leaves a tail on each pellet.
That is why bath length is specified against output rather than against available floor space. A line at 150 to 250 kg/h uses a 4 m bath and the core freezes in eight to fifteen seconds. Push 800 kg/h through the same bath and the strands leave it warm in the middle. The TL-ST-800 is supplied with a 6 m bath for exactly this reason.
The published pairings are simple: 4 m at 150 to 250 kg/h, 5 m at 350 to 500 kg/h and 6 m at 600 to 800 kg/h. Those figures assume water held between 20 and 35 degrees C and a strand that enters at a shallow angle. Change either assumption and the pairing has to be reviewed.
Water temperature is a window

Below 18 degrees C the strands become brittle and break at the first guide roll. That sounds counter-intuitive, because colder water should cool faster. The problem is thermal shock at the surface: a hard skin forms while the core is still contracting, and the stress cracks the strand at the point where it is bent.
Above roughly 40 degrees C the core does not freeze in the available length and the cutter smears. Between those limits the line has a working window, and the chiller option exists to hold it. A chiller and temperature control to plus or minus 1 degree C is listed as an option on the TL-ST precisely because ambient water varies by season and by plant.
The practical setting is found on the machine. Run at the lower edge of the window, watch the pellet faces under a lamp, and raise the temperature until the tails disappear without strand breaks. Record the number. The next operator should not have to repeat the experiment.
The air knife between bath and cutter
Strands leave the bath wet. If that water arrives at the cutter, the pellets carry a film into the bag and clump together, which is precisely the feeding problem the cubic shape was chosen to solve. An air knife strips the surface water before the feed rolls take over.
The knife position and air pressure need checking whenever the strand diameter changes. A 24-strand line needs more air than an 8-strand line, and it is one of the reasons a second air knife is offered as an option for high strand counts. Extra guide rolls are supplied with it so the strands stay separated on the way to the rotor.
A simple check is to catch a handful of pellets straight from the discharge and press them in a clear bag. If they stick together, the air knife is not doing its job or the water is too warm. If they flow freely, the drying stage is right and the next check belongs at the cutter.
Reading the bath on a running line
A well-set bath has evenly spaced strands, no steam at the entry point and no colour change along the line. Strands that cross or clump in the water usually mean the die holes are unevenly blocked, which is a screen pack problem rather than a bath problem.
The weir and overflow keep the water level stable. A falling level exposes the strands early and shortens the effective bath, so the level belongs on the operator round along with temperature. The bath pump is rated at 2.2 kW on the TL-ST, and a blocked filter on the pump circuit produces the same symptom as a short bath.
Finally, look at the pellets, not just the strands. Clean faces with a square cut mean the core was frozen and the knife clearance is right. Tails mean the bath was short or the water was warm. Dust means the knife is worn. Each symptom points to a different part of the line, and the bath is only one of them.
When the bath cannot do the job
Some polymers do not suit a long water bath. PVC cable compound and heavily filled masterbatch can be cut at the die face instead, and our underwater pelletizer handles those cases without a bath. The trade-off is a more complex cutting chamber and a circulating water loop.
For a general-purpose line running PP, PE, ABS and HIPS regrind, the bath remains the most transparent option. The operator can see the melt, and the cooling setting can be judged by eye before a single pellet is tested. That visibility is why the strand platform is still the reference line in our range.
If the plant is short of floor length, measure the real envelope before deciding. The TL-ST-400 line plus its bath occupies 10.5 m, and a water ring line doing similar output is substantially shorter. Our strand pelletizing product page gives the full dimensional table, and our auxiliary equipment page covers the chillers and conveyors that sit around the bath.
Bath length by output on TL-ST
Bath length and water temperature are set by output and polymer, not by the space available beside the die. These are the published pairings.
| Model | Output | Bath length | Line footprint |
|---|---|---|---|
| TL-ST-200 | 150-250 kg/h | 4 m | 8.5 x 1.2 m |
| TL-ST-400 | 350-500 kg/h | 5 m | 10.5 x 1.4 m |
| TL-ST-800 | 600-800 kg/h | 6 m | 12.5 x 1.6 m |
| Water range | 20-35 C working | 8-15 s in bath | Chiller option +/- 1 C |
Questions buyers ask about this machine
Q1: Why do my strands break at the first guide roll?
Water below 18 degrees C makes the strand surface brittle while the core is still contracting. The stress cracks the strand where it bends. Raise the bath temperature into the 20 to 35 degree window and check that the die is not running too cold.
Q2: What happens if the bath is too short?
The strand surface freezes but the core stays soft. The cutter then presses rather than cuts, leaving tails on the pellets and raising fines. Bath length is matched to output: 4 m at 250 kg/h, 5 m at 500 kg/h and 6 m at 800 kg/h.
Q3: Is a chiller necessary on a strand line?
Not always, but it is offered because ambient water temperature varies by season. A chiller holds the bath to plus or minus 1 degree C, which keeps pellet shape consistent through the year. Plants with stable water temperature often run without one.
Q4: How do I know the air knife is working?
Catch pellets at the discharge and press them in a clear bag. If they stick together, surface water is reaching the cutter. Check the knife position and air pressure, and add a second knife if the line runs 24 strands.
Further reading on this site: quality control.
The rest of this series covers the same equipment from different angles: Why Cubic Pellets Still Win in Injection Feeding, Strand Breaking at the Die: From Symptom to Cause, Strand Cutter Maintenance: Knife Clearance and Blades and Strand Pelletizing Line: How Much Floor Space to Plan.
About the author
Zhou Gong (周工) builds recycling lines at TENGLONG Plastic Machinery, a factory in Linyi, Shandong, with 18,000 m² of floor area, 30-plus staff and 820-plus lines delivered to 46 export markets. A soft core does not announce itself. You see it as tails on the pellets, and by then the bath setting is already wrong. The numbers in this article come from test runs and from dated published sources, not from a sales sheet.
If you want a recommendation rather than a catalogue, send the material form, the contamination level and the target output. We return a model and a price range within one working day, and the test run on 10–20 kg of your own material is free before the balance is paid.