A masterbatch formulation is a ratio between four streams: pigment, carrier, wax and additive. Loss-in-weight dosing measures the mass actually leaving each hopper and adjusts feeder speed continuously, holding plus or minus 0.3% per component on the TL-MB.
That matters because pigment bulk density changes between batches, so a volumetric feeder would hold volume while the delivered mass drifted. High-bulk powders such as talc and TiO2 can bridge at the main throat, which is why a side feeder and dust extraction are offered.
Four streams, one stable ratio
- Pigment sets colour, carrier sets let-down, wax sets dispersion and additive sets function.
- Bulk density changes defeat volumetric feeding; loss-in-weight measures real mass.
- Refill events and bridges cause most dosing faults, not calibration errors.
- Statistical process control export lets dosing data be compared with speck counts.
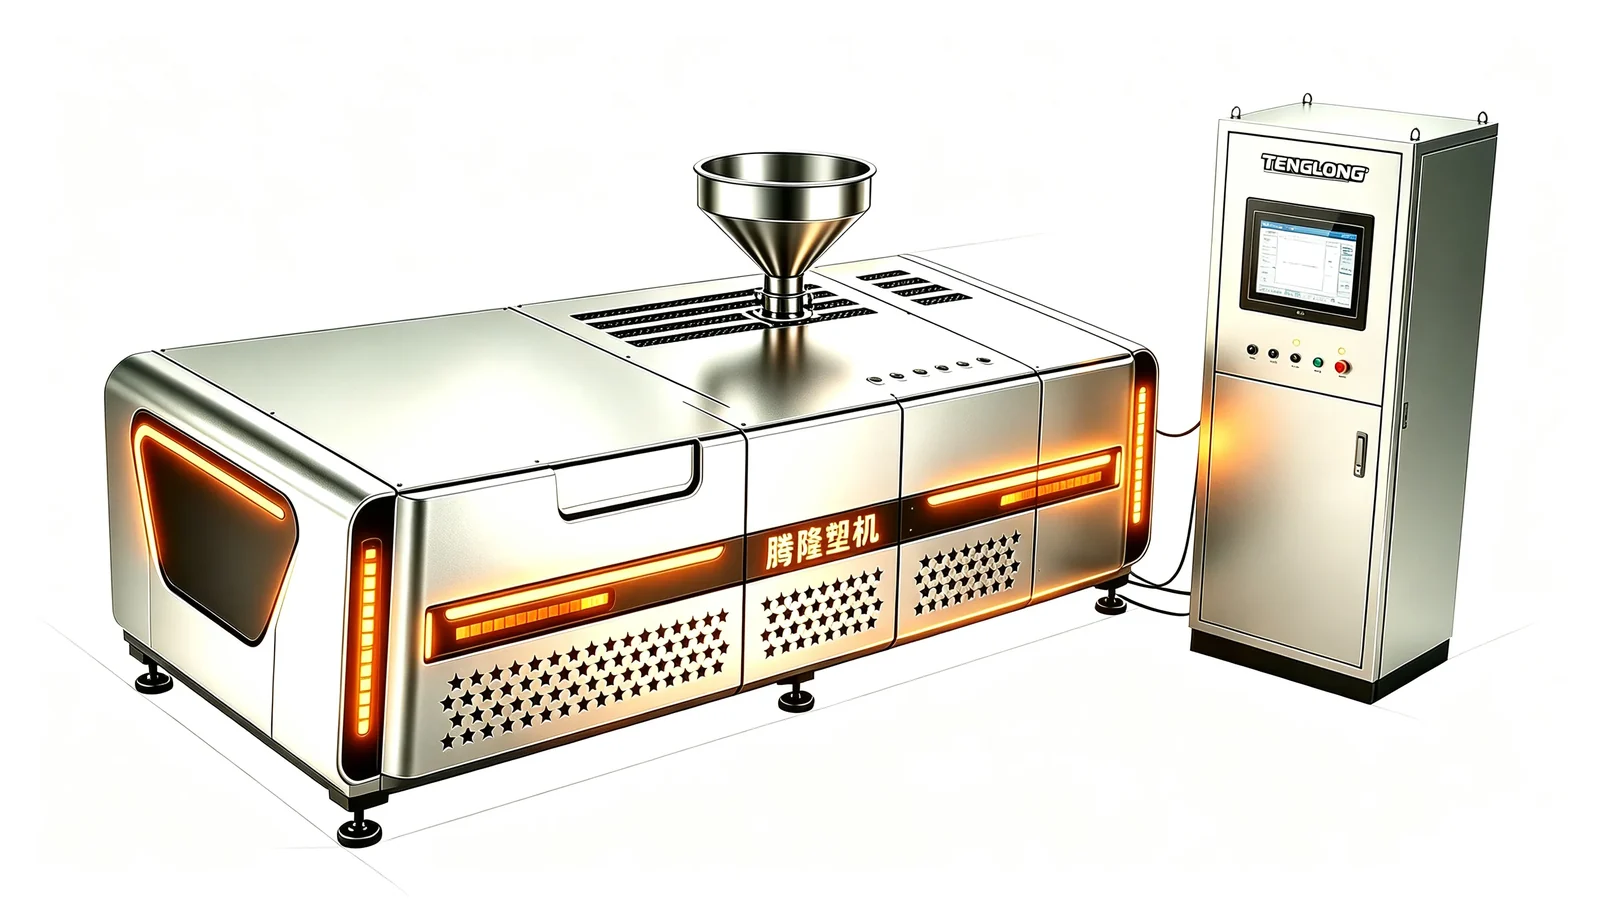
Four streams, one ratio
A masterbatch formulation is a ratio between four or more streams: pigment, carrier resin, wax and additives. If any stream drifts, the let-down ratio at the customer changes, and the colour or additive level goes with it. Volumetric feeding cannot hold that ratio because bulk density changes between pigment batches.
Loss-in-weight dosing measures the mass actually leaving each hopper per unit time. The controller compares the measured loss against the target and adjusts the feeder speed continuously. On the TL-MB the published accuracy is plus or minus 0.3% per component, which is tight enough for a 2% let-down ratio to remain predictable.
The four streams do different jobs. Pigment sets the colour, carrier carries it, wax controls dispersion and viscosity, and additives deliver the functional property. A 0.3% error in the additive stream can matter more than the same error in the carrier, so tolerances should be set per component rather than as one blanket figure.
Why bulk density defeats volumetric feeding
A volumetric feeder delivers a set volume per revolution. Pigment powders vary in bulk density with moisture, compaction and supplier, so the same screw speed delivers different mass from one sack to the next. A black masterbatch with 40% carbon black is especially sensitive because the powder is light and aerated.
Loss-in-weight feeding removes that variable. The hopper sits on a load cell and the controller measures the real mass flow, so a change in bulk density produces a change in feeder speed rather than a change in formulation. The weighing continues until the hopper is refilled, then the controller re-establishes the reference weight.
Refill events are worth watching. A poorly timed refill produces a short disturbance in the measured loss, and an operator who sees a colour band in the product should check the refill log before adjusting a temperature. Most dosing faults are refill or bridging faults, not calibration faults.
Feeding high-bulk pigments
Talc and some TiO2 grades bridge in a small hopper because their bulk density and flow behaviour differ from pelletised carrier. The TL-MB offers a side feeder for high-bulk pigment and talc, which introduces the powder downstream of the main hopper and avoids competing with the carrier at the same throat.
A vacuum loader and dust extraction on the powder port are listed as options. Dust extraction is a quality control measure as much as a housekeeping one: airborne pigment settling on the floor eventually finds its way into a different batch and shows up as a speck.
Liquid colour injection is offered for solvent-based pigment systems. It changes the dosing problem entirely, because a liquid stream can be metered by mass flow without bridging. The choice between powder and liquid feeding belongs in the formulation design, not in the machine purchase.
Tying dosing to dispersion
Dosing accuracy and dispersion are separate problems, but they interact. A pigment stream that surges by 2% for a few seconds creates a local concentration spike that the dispersion zones may not break down properly. The result is a band of specks rather than a uniform increase.
That is why the TL-MB combines gravimetric dosing with a 40:1 twin screw and two dispersion zones. Steady input lets the shear history stay steady. If the feed surges, even a good dispersion section produces an inconsistent product, because residence time at a given composition has changed.
Statistical process control export is offered as an option, which lets the dosing data be reviewed against the speck count from the lab. A correlation between a feeder disturbance and a speck band is easy to see when both records share a timestamp, and hard to see when they do not.
Setting the tolerances
Start from the customer’s let-down ratio. A 2% let-down means the pigment concentration in the masterbatch has to be accurate enough that a 2% addition lands within the customer’s colour tolerance. Work backwards from that requirement to a per-stream tolerance instead of accepting the machine’s nominal figure.
Then set a tolerance for the additive stream, which often has the narrowest effective window. Flame retardant and UV packages are usually specified in a tight band by the end user. An additive that is 0.3% low in the masterbatch becomes a much smaller error at let-down, but the specification still belongs on the masterbatch.
Record the actual dosing drift over a full shift and include it in the acceptance test. Our factory test procedure is described on the quality page, and a dosing trial on the customer’s own powder is a reasonable request before balance payment. powders differ more than machine specifications suggest.
Four gravimetric streams and what they control
Four streams have to land inside tolerance at the same instant. These are the gravimetric targets and what each one controls.
| Stream | Published accuracy | Controls |
|---|---|---|
| Pigment | +/- 0.3% | Colour strength, speck risk |
| Carrier resin | +/- 0.3% | Let-down ratio, viscosity |
| Wax | +/- 0.3% | Dispersion, melt viscosity |
| Additive | +/- 0.3% | Functional property window |
| High-bulk powder | Side feeder option | Bridging and surge control |
What buyers ask us before they order
Q1: Why not use volumetric feeders on a masterbatch line?
Pigment bulk density changes between batches with moisture and compaction. A volumetric feeder holds volume per revolution, so the mass changes. Loss-in-weight dosing measures mass leaving the hopper and holds the ratio to plus or minus 0.3% per component.
Q2: What causes a colour band in the finished pellets?
Often a feeder refill or a bridged powder hopper rather than a temperature problem. Check the refill log and the load-cell trace before changing the barrel profile. A side feeder is offered for high-bulk pigments and talc that bridge at the main throat.
Q3: Does dosing accuracy affect dispersion?
Yes. A pigment surge creates a local concentration spike that the dispersion zones may not break down, producing a band of specks. Steady gravimetric input lets the shear history stay steady and the product remain uniform.
Q4: How tight should my dosing tolerance be?
Work backwards from the customer’s let-down ratio and colour tolerance rather than accepting a blanket figure. Additive packages such as flame retardant often need the narrowest window, so set tolerances per stream.
The pages that come up most often alongside this one: the pellets glossary.
The companion write-ups for this machine family are: Masterbatch Dispersion: Why 20 Microns Decides Quality, Masterbatch Colour Change in 40 to 60 Minutes, How Much TiO2 Can a Masterbatch Granulator Carry and Minimum Masterbatch Batch Size: 25 kg on the MB-35.
About the author
Zhou Gong (周工) builds recycling lines at TENGLONG Plastic Machinery, a factory in Linyi, Shandong, with 18,000 m² of floor area, 30-plus staff and 820-plus lines delivered to 46 export markets. When a colour band appears in the pellets, check the feeder refill log before touching a temperature. The numbers in this article come from test runs and from dated published sources, not from a sales sheet.
If you want a recommendation rather than a catalogue, send the material form, the contamination level and the target output. We return a model and a price range within one working day, and the test run on 10–20 kg of your own material is free before the balance is paid.