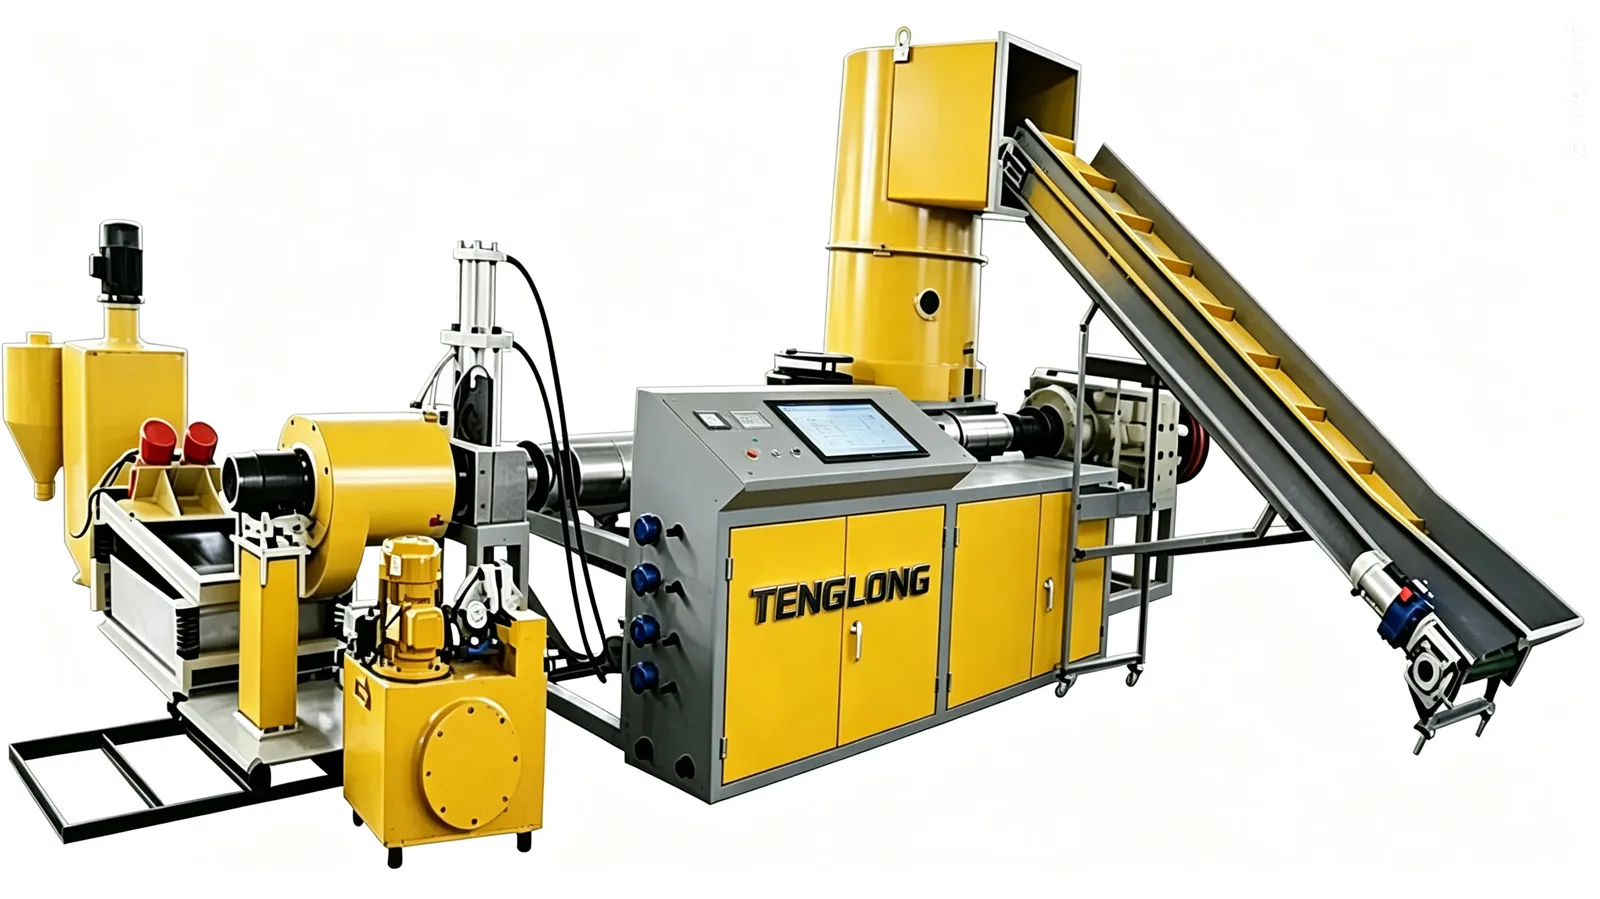
Summary: This is a symptom-first troubleshooting playbook for the TL-TS twin screw granulator: symptom, then likely cause, then the action that actually settles it. Six faults account for almost every call we take on a compounding line, and none of them arrive labelled: torque climbing into the limiter, feed bridging at the throat, melt temperature swinging between zones, colour specks and uneven shade, glass fibre shorter than specified, and bubbles caused by moisture in the filler. Each entry is tied to a published machine figure you can check yourself: the 190–260 °C barrel zones, the torque limiter and melt-pressure trip, the eight dosing channels at ±0.5%, the zone-8 vacuum vent, the 60–120 bar melt pump and the 60–80 mesh screen pack, and the per-minute PLC trend that shows the fault developing before the pellets show it.

Order of operations: contain it, then isolate it
The first decision is not a setting, it is whether this line should be running at all. A gearbox that has tripped on the torque limiter or the melt-pressure trip has already protected itself, and pushing past it converts a control event into a gearbox rebuild. Once the machine is safe, move exactly one setting. Two settings moved together produce a result you cannot attribute to either one.
Read the trend before touching a knob
The second habit is to read the trend first. Every unit in our factory runs 24 hours no-load and then 4 hours on the customer’s material, with output, melt pressure, melt temperature and kWh logged every minute. The same logging on your own line turns a vague complaint into a signal: rising melt pressure with falling output means the screen pack is closing; rising torque at constant feed means the material changed. The procedure is described on how every line is factory tested.
Then work down the physical order of the process — feed, melting, mixing, venting, filtration, cut — because a fault earlier in that chain reappears later as a different symptom. Start from the published figures: the TL-TS twin screw granulator specification lists them model by model, and the vocabulary is in the pellets and feedstock glossary.
Torque climbs and the gearbox trips
- Symptom — the torque reading climbs toward the limiter, the gearbox trips on a cold start, output falls at constant feed rate, and melt temperature rises at the same time.
- Cause — four usual sources. A cold start with a full barrel of material the screw has to push, which is exactly what the published torque limiter and melt-pressure trip exist to catch. A filler load above the recipe, or the wrong screw set for that recipe. Moisture in the feed turning to steam in the barrel. And wear on the kneading elements, or a screen changer that is slow to close.
- Action — warm the barrel to the published zone band of 190–260 °C and purge before restarting, because a cold start is a protection event, not a fault. Then compare actual torque against the limiter setpoint and check the recipe against the published capability of 70% calcium carbonate and 30% glass fibre. Check moisture in the feed and filler, then check the screen pack and the hydraulic screen changer. Never raise the limiter setpoint to stop a trip: it is the last line of protection before the gearbox.
Feed bridging and dosing drift
- Symptom — output falls while the set feed rate stays the same, one dosing channel reads high or low, the side feeder stalls, and the loss-in-weight feeders report a sudden demand change.
- Cause — bridging at the feed throat with flake that has fused into a plug is the common one. A loss-in-weight feeder bridged or a vacuum loader starved behaves the same way. A side feeder can also stall because the pressure profile around it has changed: the zone-8 vent and the melt pump both alter the pressure the side feed works against, so a vent adjustment can starve a side feeder that was fine yesterday.
- Action — open the feed throat and look for a packed plug, and check the hopper level. Then verify each channel against its ±0.5% target on the HMI, and check the side feeder throat and the refill path. Before changing the recipe, confirm that the zone-8 vent and the melt pump have not been adjusted since the last stable run. Recipe management and batch traceability on the S7-1500 let you compare channel drift between batches, which separates a dosing problem from a material problem in minutes.
Melt temperature swinging between zones
- Symptom — zone temperatures oscillate, melt temperature swings between the barrel and the die, shade changes between bags of the same batch, and melt pressure wanders around its setpoint.
- Cause — the barrel has six independently cooled zones, so a zone fighting the screw speed is the usual source, and one setpoint copied across every zone is a setpoint that is wrong in most of them. A screw set with too many kneading blocks for the recipe generates more shear than the melt can absorb. A cold filler stream dropping from the side feeder straight into the melt pulls the local temperature down. A failed thermocouple or heater and a blocked deep-groove cooling bore produce the same symptom with different causes.
- Action — compare every zone against the published 190–260 °C band and check that the profile follows the recipe rather than repeating one number. Check the side feeder injection point temperature. Verify the thermocouples against a handheld instrument. Confirm that the deep-groove cooling bores are clear, because those bores are what allow one zone to run hotter than the next. Where a melt pump is fitted, watch the 60–120 bar band: a pressure swing reaches the die as a temperature swing.
Colour specks, shade drift and broken glass fibre
- Symptom — visible colour specks in a thin film, shade drifting batch to batch outside tolerance, agglomerates inside the pellet, and glass fibre shorter than the specified length.
- Cause — these are two different faults with two different mechanisms, and they get confused constantly. Specks and shade drift are wetting problems: the element layout does not renew enough surface, the filler enters before it is wetted, or the wrong screw set is running. Short fibre is a shear problem: the geometry is cutting the fibres instead of carrying them. Worn elements make it worse, because a smoothed kneading block smears less.
- Action — check the element layout against the recipe first, because segmented screws are configured per recipe and the layout is part of the specification. Confirm that talc, glass fibre and CaCO3 are side fed rather than dropped in with the base polymer, and that the liquid injection port is used where silane, oil or flame retardant is in the recipe. Confirm the eight channels are holding ±0.5% before you blame the screw. For abrasive grades, check that PM-HIP elements and bimetallic barrel sleeves are fitted, since a worn element changes the mixing behaviour before it changes anything visible. The published dispersion target for a compound sold into thin film is below 20 µm, and that is the number to measure against.
Short fibre and visible specks are two different faults
The most common mistake here is treating a speck as a fibre problem or a fibre problem as a wetting problem. One test separates them: break a pellet and look at the fracture surface. Agglomerates in the matrix are a wetting failure and will not respond to element geometry. Fibres pulled short and lying loose are a shear failure and will not respond to better wetting.
Moisture, foam and bubbles from the filler
- Symptom — bubbles inside the pellets, spitting at the die, foam on the strand, pellet weight varying run to run, and a vacuum load that has crept up without a change in recipe.
- Cause — moisture arriving with the filler instead of being removed at a vent. A vent that is not pulling, whether through a leak, a blocked line or a wrong zone setting. Volatile content in recycled feedstock. Air drawn in at an unsealed feed throat or around a side feeder. And a melt pump that is flooded rather than starved, which shows as a wandering pressure rather than a clear fault.
- Action — measure moisture in the filler and in the base feed first. Then check the zone-8 vacuum vent for vacuum level and the line for leaks, and confirm that the vent sits downstream of where the filler enters the melt. Check that the feed throat and the side feeder are sealed so air is not pulled in. The published answer to genuinely high volatile levels, 5,000 ppm, is two-stage devolatilisation at high surface renewal; a single vent position will not get you there, so if the number is structural rather than seasonal, the configuration is the fix.
Moisture in a filler is a different problem from moisture in a polymer
A polymer that arrives wet usually means the dryer upstream is not doing its job, and that is a drying question. A filler that arrives damp is a compounding question, because the filler is metered in separately and enters at a side feeder position where it can pick up moisture from the feed itself. Check the two separately and measure both. For heat-sensitive grades the same removal of water at a controlled temperature is covered in PET intrinsic viscosity loss.
| Symptom | Most likely cause | First check | Corrective action |
|---|---|---|---|
| Torque climbs into the limiter, gearbox trips on cold start | Cold start with a full barrel, filler load above the recipe, feed moisture, worn elements | Actual torque against the limiter setpoint, zone temperatures against 190–260 °C | Warm and purge before restart, then correct the recipe, moisture or wear; never raise the limiter setpoint |
| Output falls at constant feed, one dosing channel drifts | Feed throat bridging, a bridged loss-in-weight feeder, side feeder starved by a changed pressure profile | Feed throat and hopper level, each channel against ±0.5%, side feeder throat | Clear the plug, restore refill, and check whether the zone-8 vent or melt pump setting changed |
| Zone temperatures oscillate, shade changes between bags | One setpoint copied across six zones, too many kneading blocks, cold side-fed filler, failed heater or blocked cooling bore | Each zone against the 190–260 °C band, thermocouples against a handheld, cooling bore flow | Rebuild the profile per recipe, verify the thermocouples and clear the bores; check the 60–120 bar melt pump band |
| Colour specks, shade drift, agglomerates in the pellet | Element layout not matched to the recipe, filler not side fed, wrong screw set, smoothed wear elements | Element layout against the recipe, side feeder in service, channel accuracy, dispersion target below 20 µm | Reconfigure the elements, restore side feeding and liquid injection, fit PM-HIP elements and bimetallic sleeves for abrasive grades |
| Glass fibre shorter than specified | Shear level too high: element geometry, screw speed, or too many mixing stages for the fibre length | Element sequence for fibre grades, screw speed, fill level in the mixing zone | Change the element layout to conveying rather than kneading where possible, and reduce mixing duty |
| Bubbles, spitting at the die, foam on the strand | Moisture in the filler, a vent not pulling, air ingress at an unsealed feed, volatiles in recycled feedstock | Moisture of feed and filler, zone-8 vent vacuum level, leaks at feed and side feeder | Dry the feed, restore vent vacuum and sealing; two-stage devolatilisation is the published answer for 5,000 ppm |
Frequently asked questions
Q1: Why does the gearbox trip on a twin screw granulator, and what should I do first?
The published protection on the TL-TS is a torque limiter and a melt-pressure trip, both of which catch a cold start where the screw pushes a full barrel of cold material. Warm the barrel to the published 190–260 °C zone band, purge, and restart. If the trip returns at temperature, look at filler load, feed moisture and wear elements, and never raise the limiter setpoint to stop it.
Q2: What causes torque to climb while the feed rate stays constant?
Usually the material, not the machine: filler load above the recipe, moisture turning to steam, or the wrong screw set running. The published capability covers 70% calcium carbonate and 30% glass fibre, so a recipe above those numbers will load the screws. Check the torque trace on the PLC log before changing anything, because rising torque at constant feed is a different signal from falling output at constant torque.
Q3: Why is my colour shade drifting between batches when dosing accuracy is ±0.5%?
Because dosing accuracy is not shade tolerance. The eight gravimetric channels hold each component within ±0.5%, which protects the recipe, but dispersion decides the shade. Check the element layout against the recipe, confirm that filler is side fed rather than dropped into dry powder, and measure against the published dispersion target of below 20 µm for a compound sold into thin film.
Q4: How do I know whether short glass fibre is a mixing problem or a shear problem?
Short fibre is a shear problem: the elements are cutting the fibres instead of carrying them. Specks and agglomerates are a wetting problem: not enough surface renewal, or filler entering dry. Two different mechanisms, two different fixes. For fibre grades, change the element layout toward conveying in the mixing zone, and confirm that abrasive grades are running PM-HIP elements and bimetallic barrel sleeves rather than a worn standard set.
Q5: What is the right response when bubbles appear in the pellets?
Find where the moisture is entering rather than raising the temperature. Measure moisture in the filler and the base feed, check that the zone-8 vacuum vent is pulling to its level with no leaks, and confirm the feed throat and side feeder are sealed. If the volatile level is structural rather than seasonal, the published answer to 5,000 ppm is two-stage devolatilisation at high surface renewal.
Engineer’s note
Most of the faults on this machine come back to two things: the screw elements and how the machine is aligned. We nitride our own screws to a 0.5–0.7 mm case at HV 900–1000 and straighten them to 0.03 mm runout over the full length, and barrel, screw, gearbox and frame are aligned to 0.05 mm before the test run. When a customer reports torque climbing, I ask for the melt pressure trace first, because the trend explains more than the complaint does.
Engineering note: the numbers on this page are our own published reference ranges for the machine family, not a specification guarantee for any individual unit. Final output, specific energy and pellet quality are set by the incoming material, its moisture and contamination level, and the screen pack fitted. We write the confirmed figures onto the quotation after a factory test run on your own material.
Who wrote this
Zhou Gong (周工) is a senior plastic machinery engineer at TENGLONG Plastic Machinery in Linyi, Shandong. The factory was registered as Linyi Hedong District Tenglong Plastic Machinery Factory on 7 June 2016 and grew out of a screw and barrel workshop, so his work is rooted in the parts that decide whether a granulator holds output: screw geometry, nitriding case depth, barrel alignment and melt filtration. He prepares the technical specification for customer quotations, reviews the four-hour factory test data before shipment, and runs commissioning support on site. Screws are nitrided in-house to a 0.5–0.7 mm case at HV 900–1000 and straightened to 0.03 mm runout over the full length; barrel, screw, gearbox and frame are aligned to 0.05 mm before the test run.
Figures quoted here are engineering reference ranges published on our own product pages, not guaranteed values for any specific machine. Real output, specific energy and pellet quality depend on the incoming material, its moisture and contamination level, and the screen pack fitted. Final values are written after a factory test run on the customer’s own material, and the PLC-logged test report ships with the machine. For a quotation that reflects your material, send the feed form, contamination level and target output and a configuration comes back within one working day.
Send the fault description, the material and the PLC trend to the quotation request form and we will work through the playbook with you, then quote the parts and the configuration change needed to settle it within one working day.